mayne pharma australia
From concept to
commercialisation.
End-to-end pharmaceutical development and commercial manufacturing, delivered from our GMP-accredited South Australian facility.
our capabilites
Contract Manufacturing
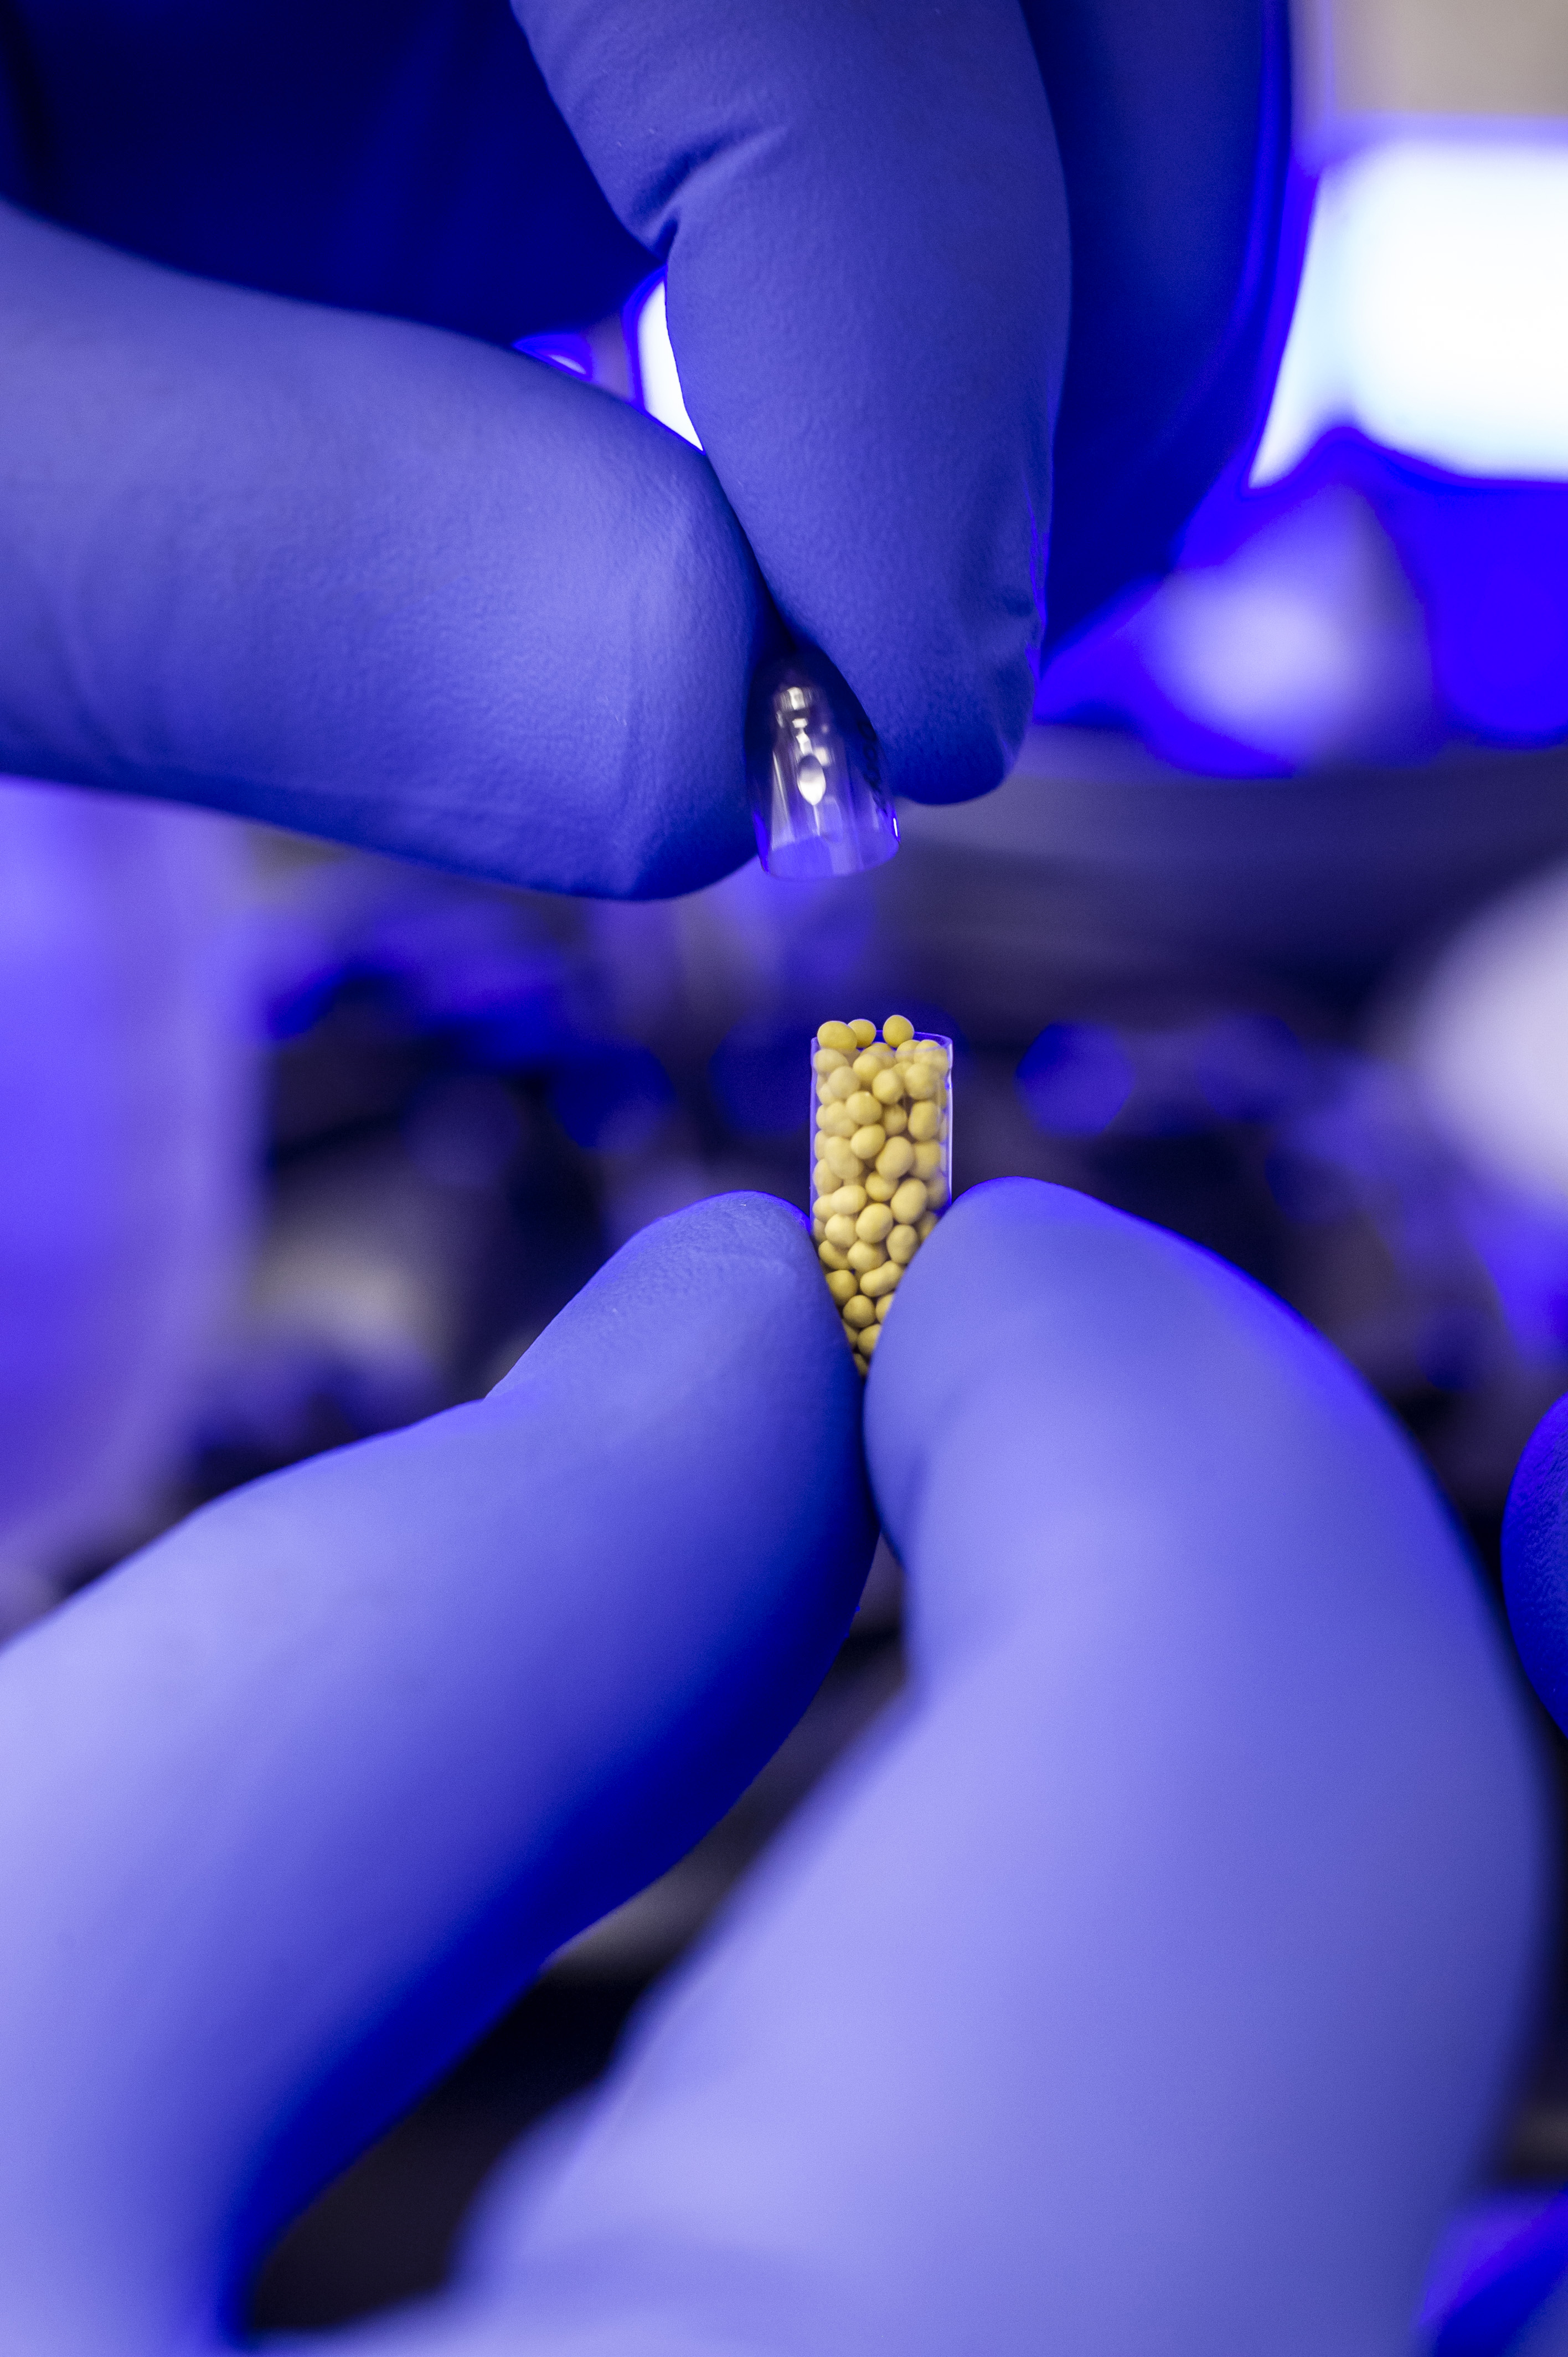
Commercial production built around your product.
For established products, technology transfers and new commercial launches requiring reliable manufacture, quality oversight and packaging support.
- Commercial production
- Technology transfer
- Validation services
- Packaging and logistics
Development Capabilities
Specialist expertise from early development to scale-up.
For pharmaceutical companies developing new products, improving existing formulations or preparing products for clinical and commercial manufacture.
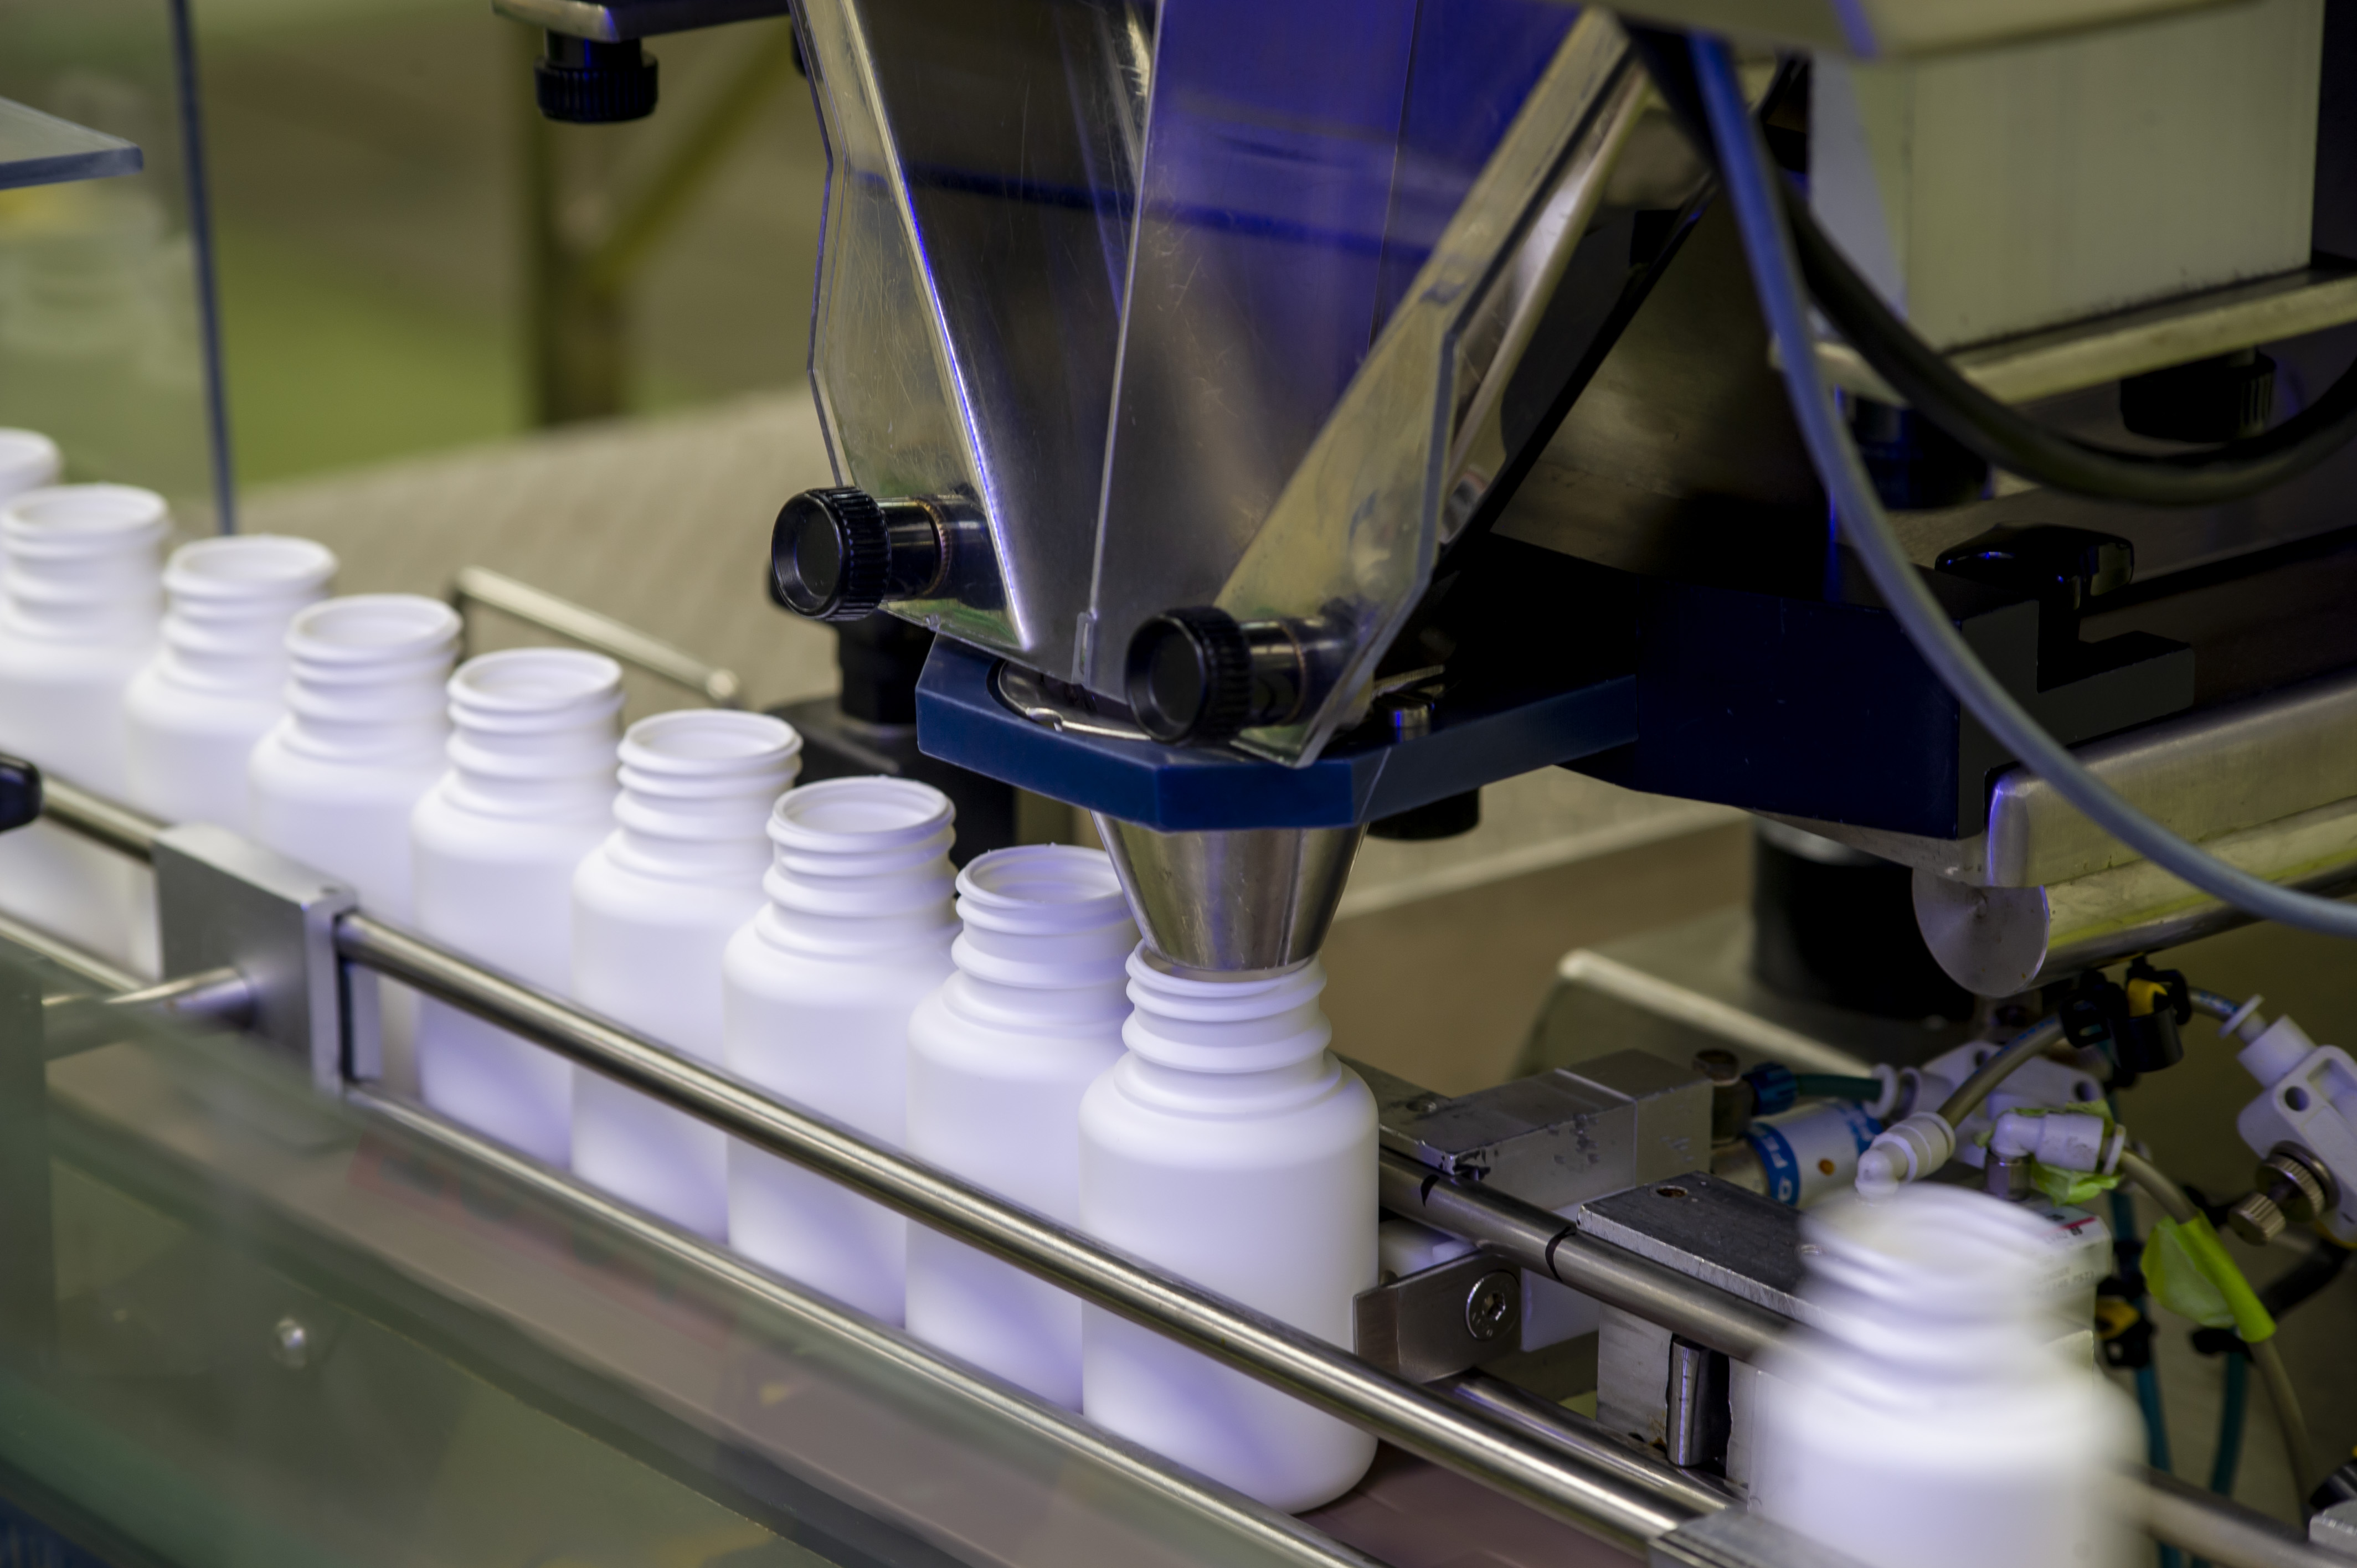
- Pharmaceutical development
- Analytical development
- Specialty technologies
- The Australian Edge
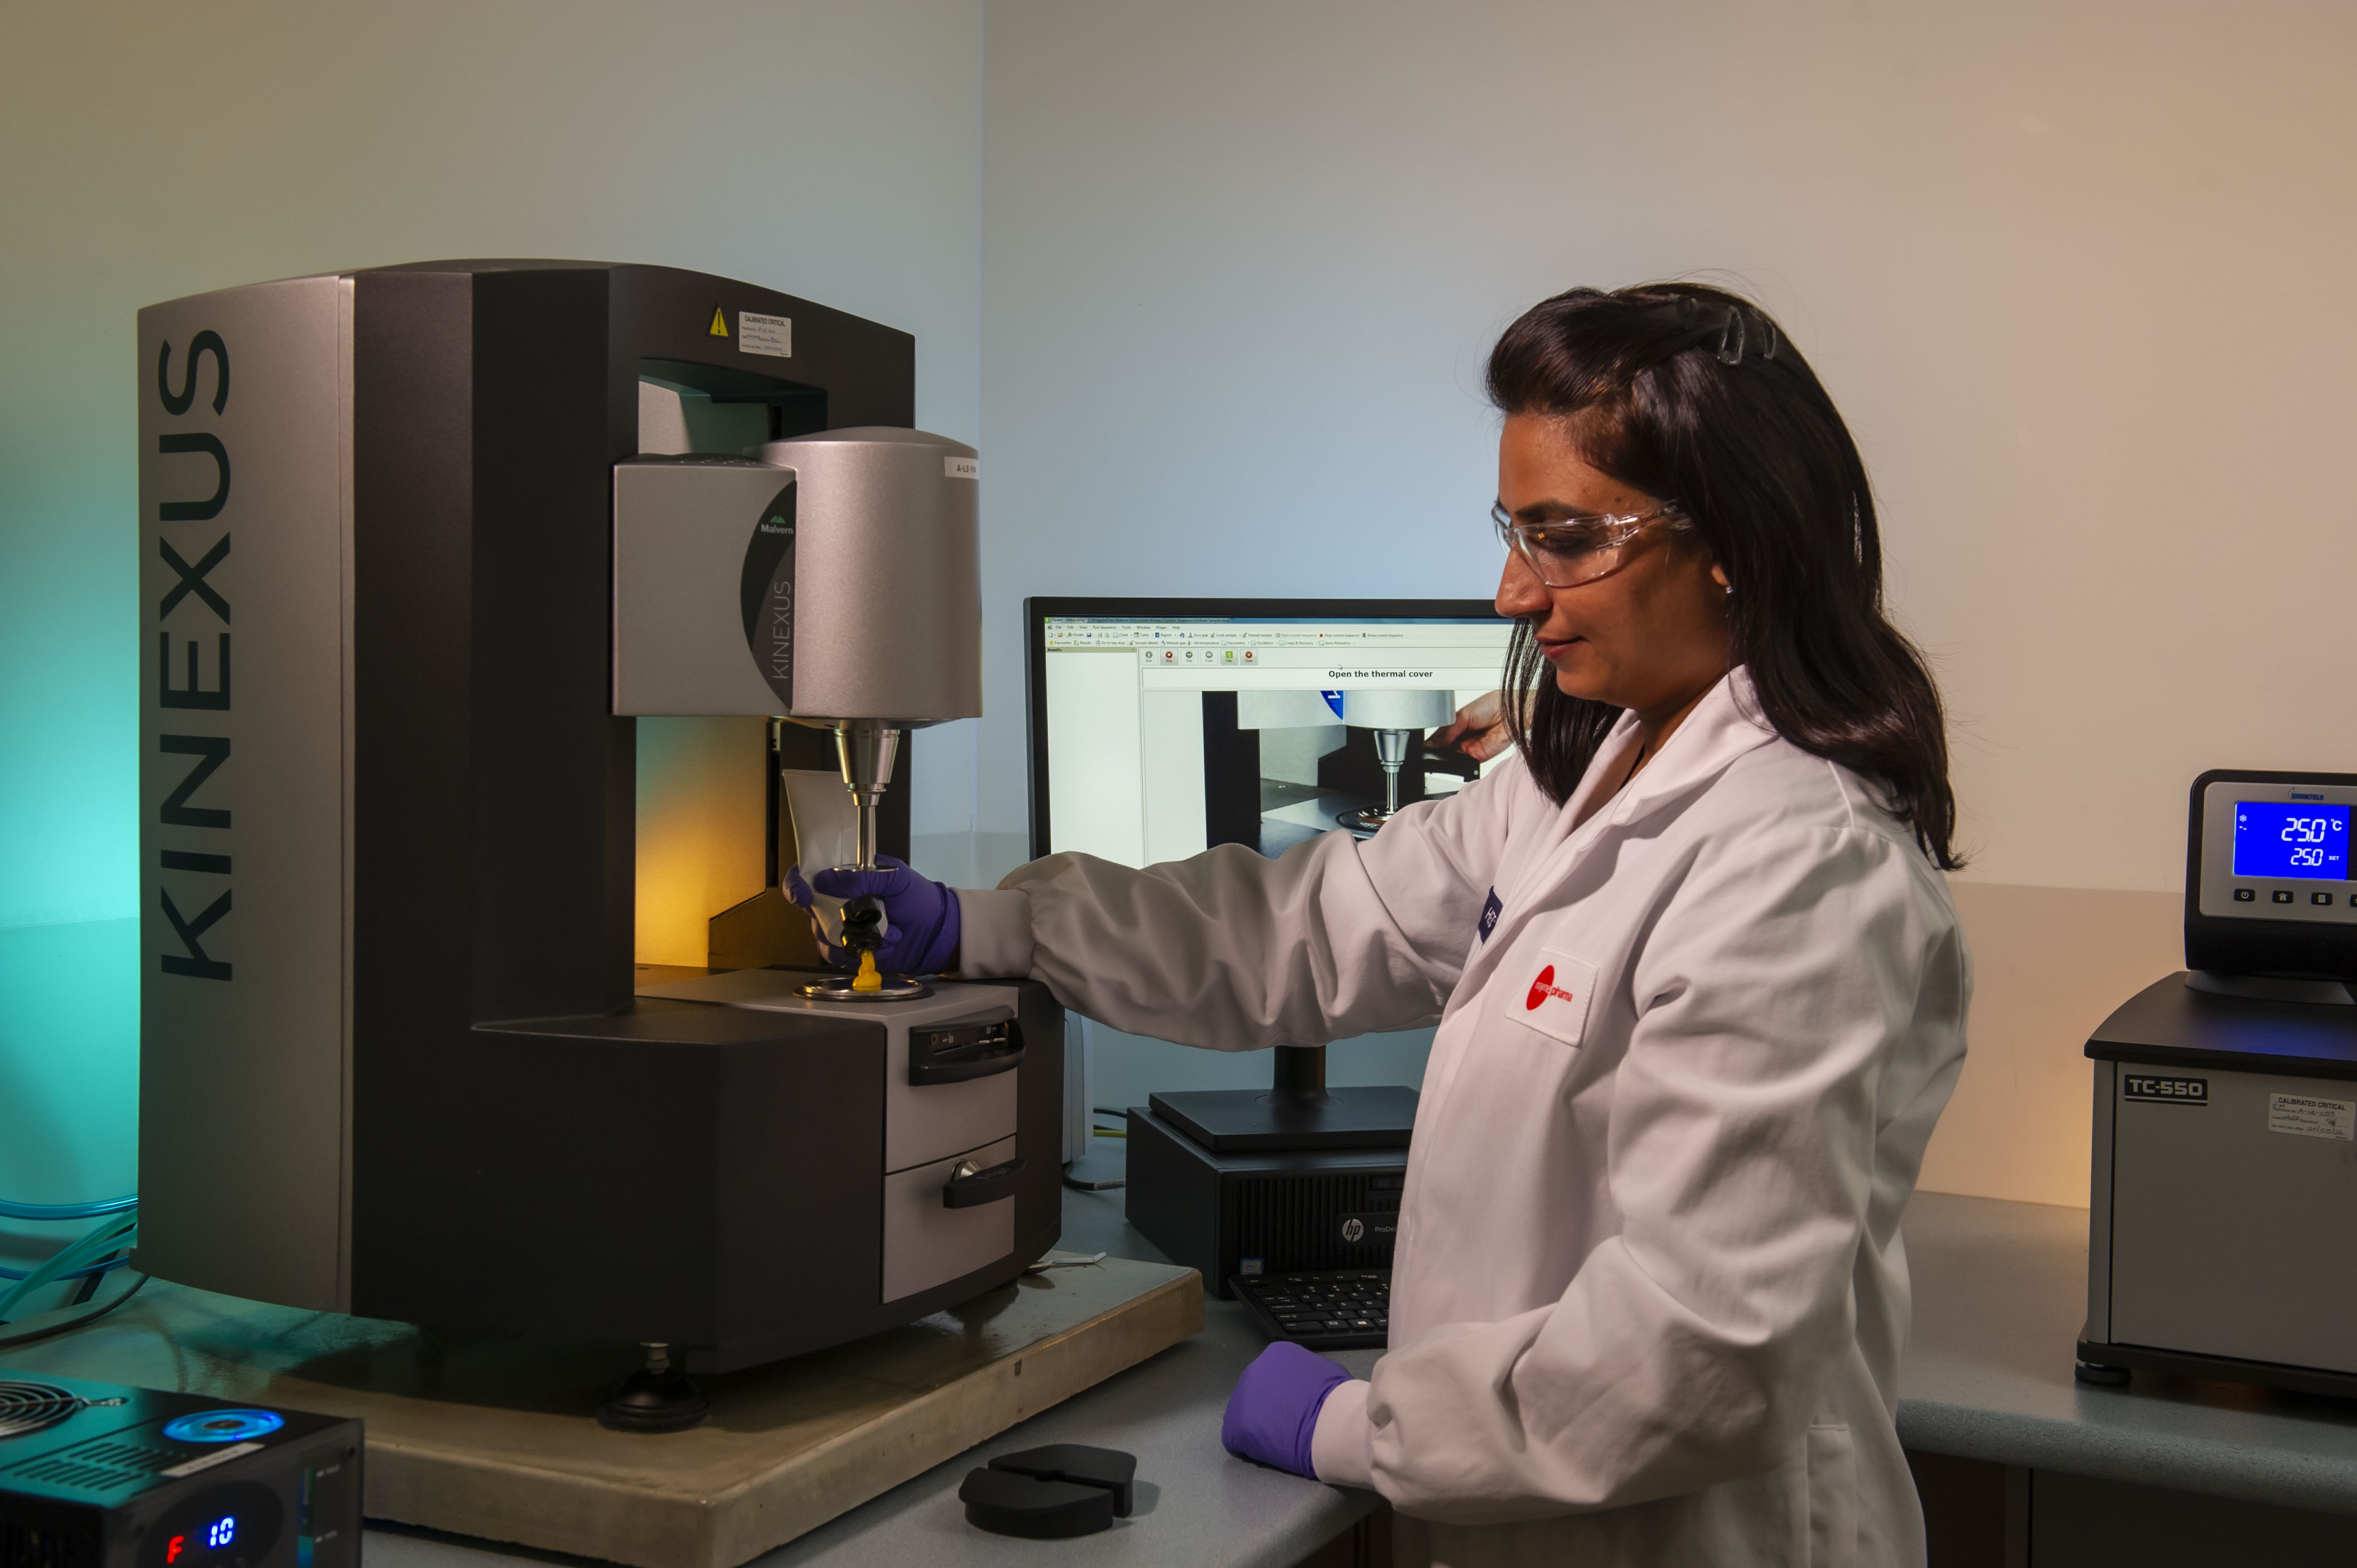
We support pharmaceutical projects at every stage — from formulation development and analysis through registration, technology transfer and commercial manufacture.
Delivered from our GMP-accredited South Australian facility, our integrated team helps reduce transfer risk, accelerate timelines and meet international quality and regulatory standards.
why mayne pharma australia
A trusted partner from development through delivery.
Specialist facilities, experienced people and global regulatory capability — all working together from one Australian site.

End-to-end capability
From formulation and analytical development through scale-up, manufacture and packaging.

Global compliance
TGA and FDA accreditation, with access to major international regulatory markets.

Experienced teams
Dedicated project management supported by a long-tenured scientific and technical workforce.

Reduced transfer risk
Development, testing and manufacturing capabilities co-located on a single site.
proven at scale
Built for complex pharmaceutical production.
Mayne Pharma combines specialist development expertise with significant annual manufacturing and packaging capacity.
start a conversation
Ready to move your
pharmaceutical project
forward?
Talk to our Australian team about your development, manufacturing or commercialisation requirements.